Hydrogen Recovery, Green and Blue Hydrogen
Engineering hydrogen solutions for today's operations and tomorrow's energy systems — recovering, purifying and producing hydrogen across conventional, blue and green applications.
One process, engineered as a whole
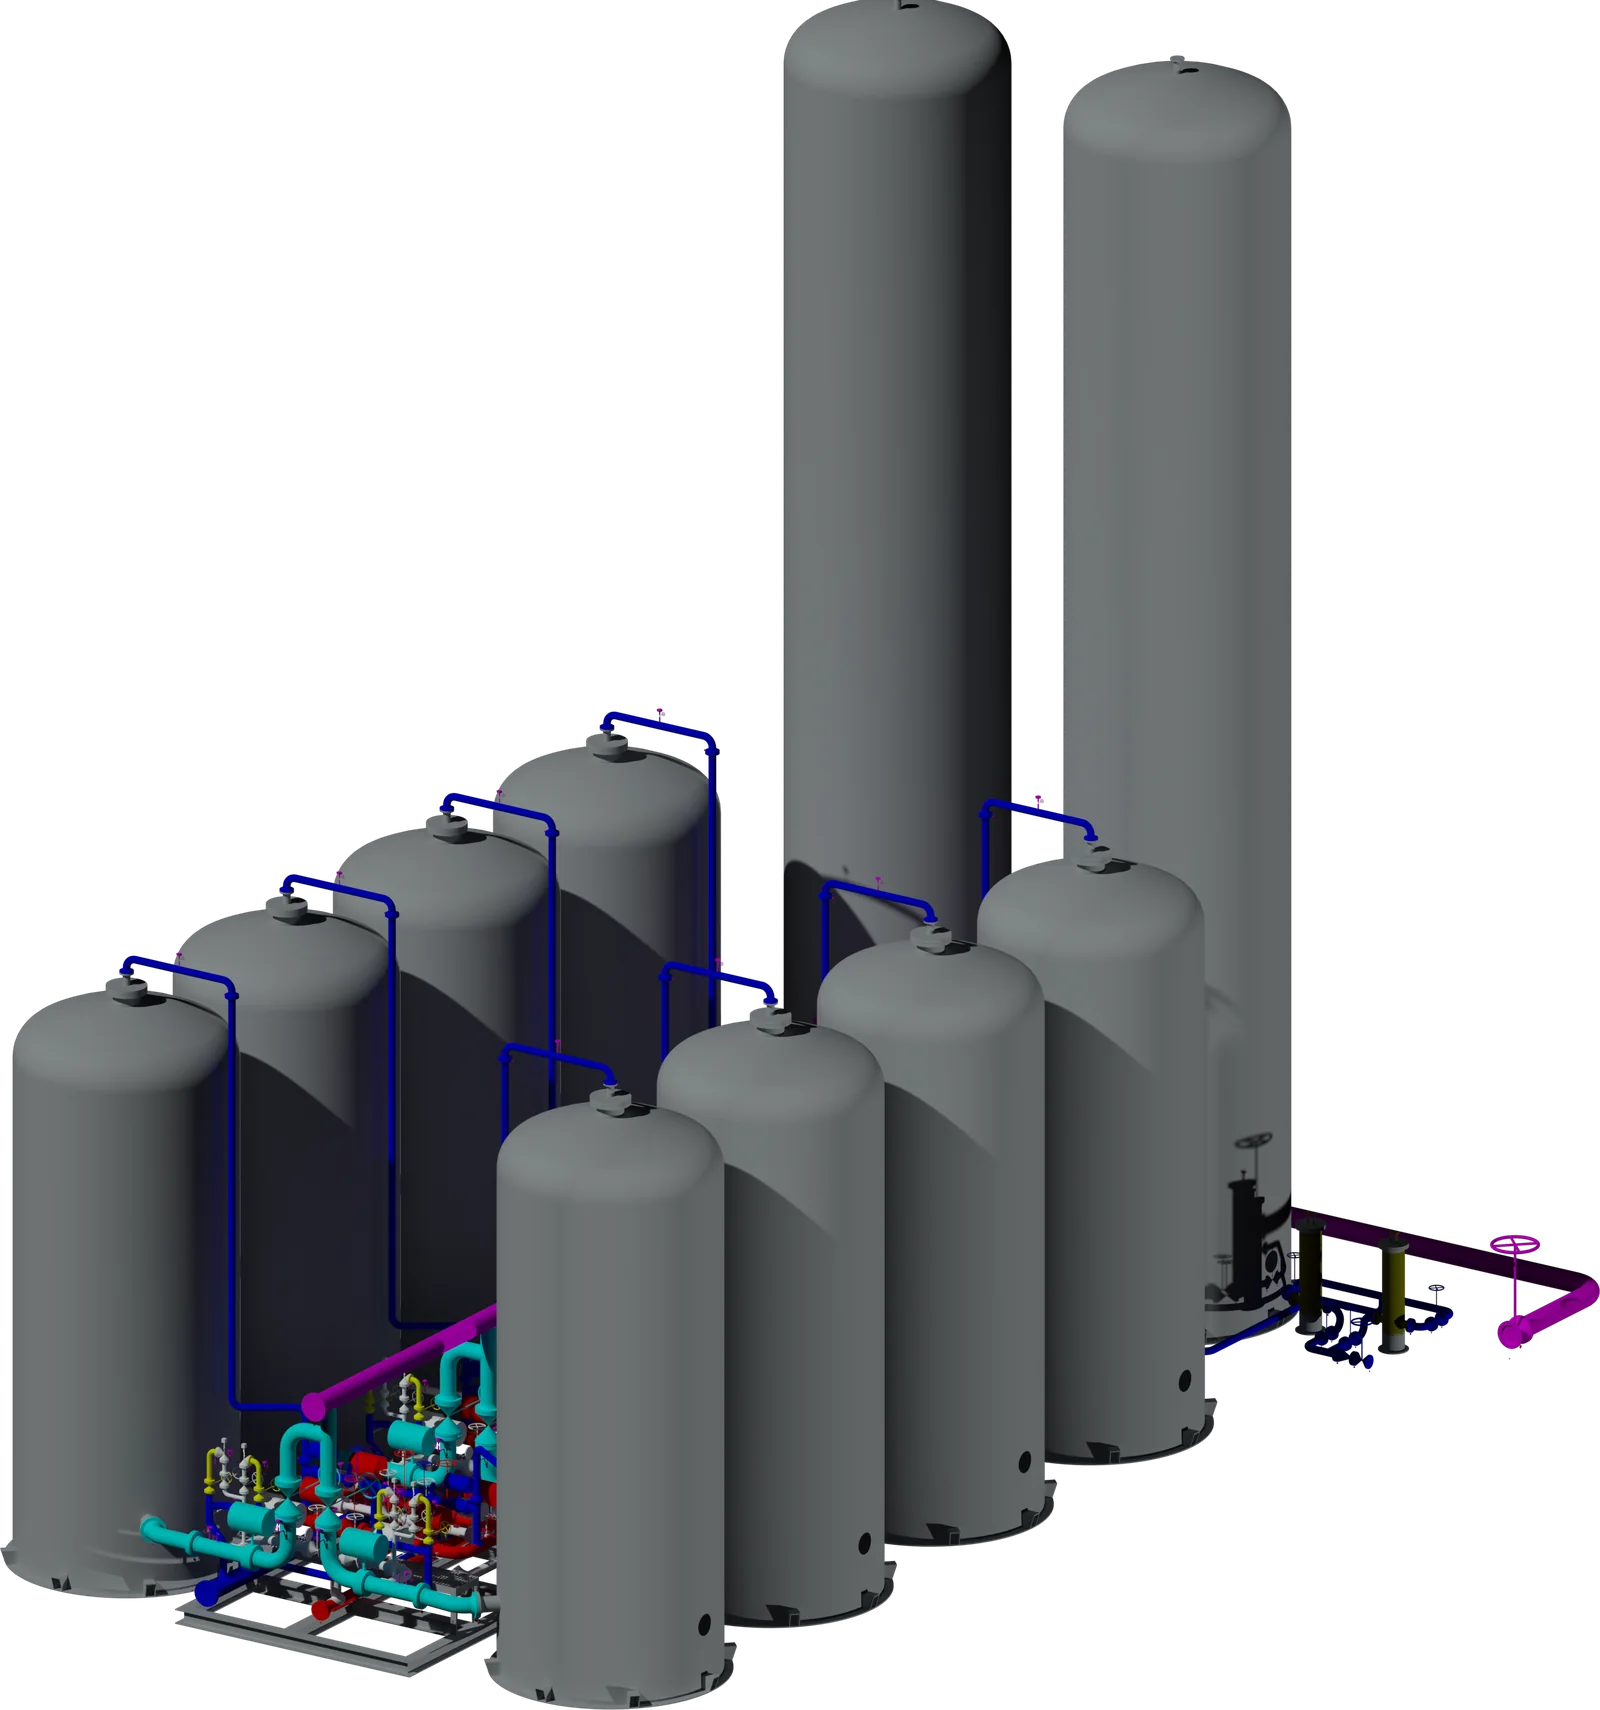
Howe-Baker provides integrated engineering solutions for hydrogen recovery, purification and production, supporting conventional, blue and green hydrogen applications. From recovering valuable hydrogen from refinery and petrochemical process streams to purifying electrolyser-produced hydrogen and improving existing hydrogen plants, our technologies are engineered around efficiency, purity, reliability and long-term plant performance.
Hydrogen projects rarely depend on a single piece of equipment. Production, recovery, purification, energy efficiency, plant capacity and downstream requirements must work together as one process. Howe-Baker combines decades of experience in hydrogen process engineering with proven technologies including Pressure Swing Adsorption (PSA), Temperature Swing Adsorption (TSA), catalytic deoxygenation and steam reforming — supporting new hydrogen facilities as well as the expansion, modernisation and optimisation of existing plants.
Hydrogen Recovery · Green Hydrogen · Blue Hydrogen
Hydrogen Recovery
Recover and purify hydrogen from refinery, petrochemical and industrial process streams using PSA technology.
ExploreGreen Hydrogen
De-Oxo and TSA purification of electrolyser-produced hydrogen to fuel-cell-grade purity.
ExploreBlue Hydrogen
Round furnace steam reforming integrated with high-performance PSA for lower-carbon hydrogen production.
Explore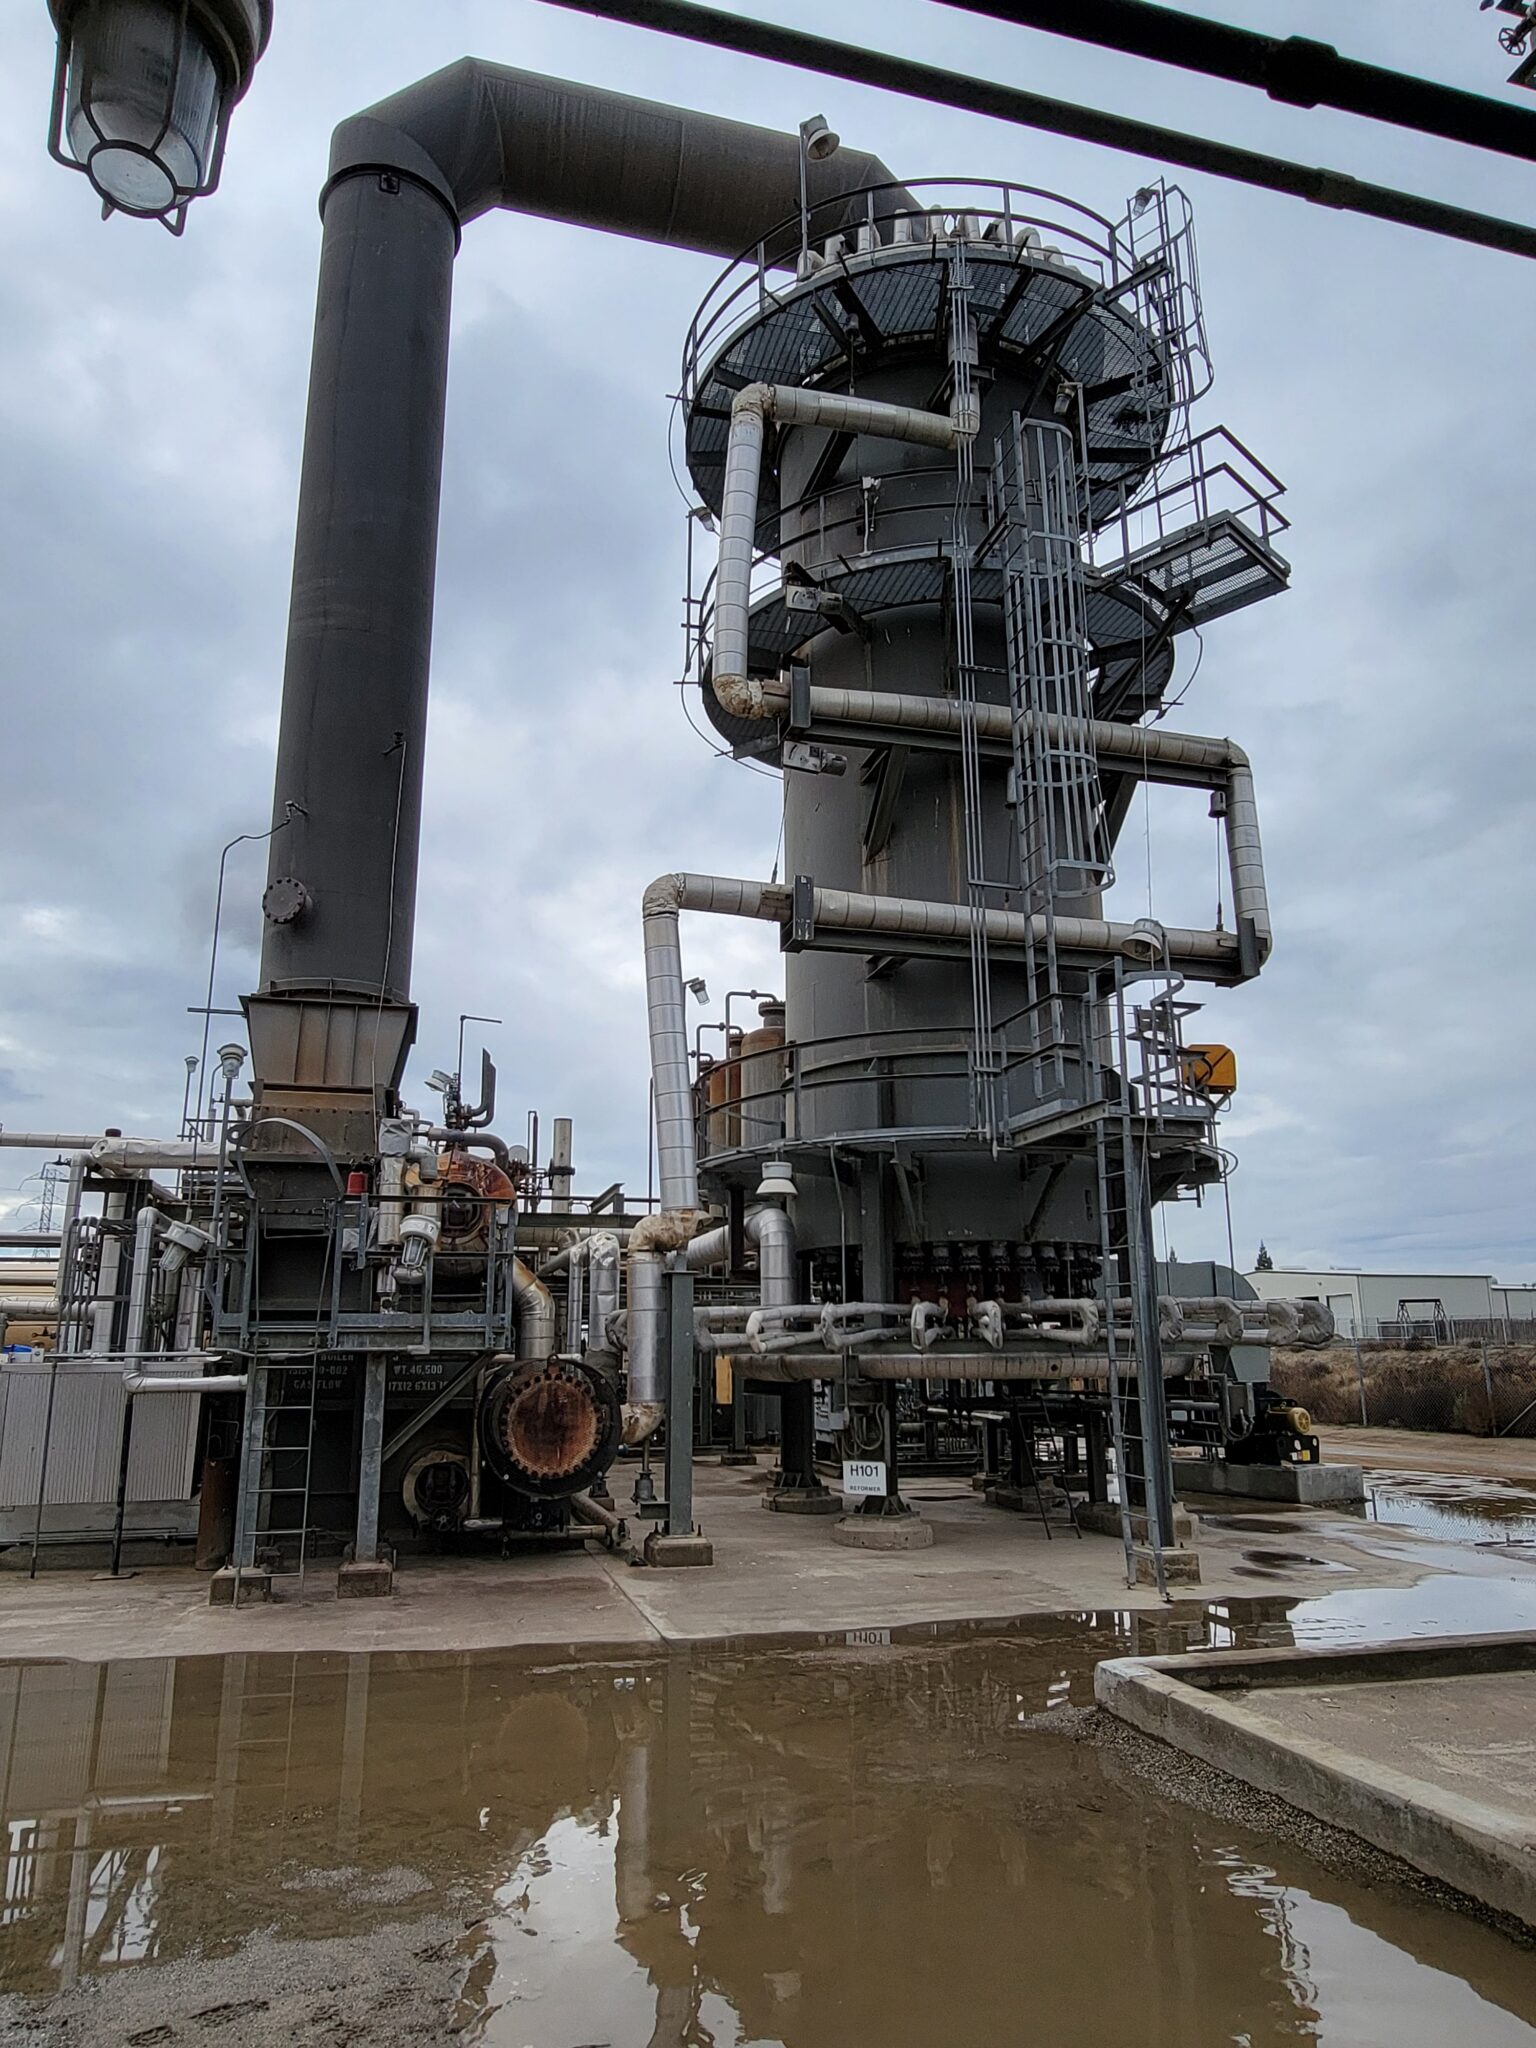
Recover more value from existing process streams
Hydrogen-rich streams within refineries, petrochemical facilities and industrial processes can contain significant quantities of recoverable hydrogen. Rather than allowing this valuable resource to enter fuel systems or be lost within the process, Howe-Baker PSA technology can recover and purify hydrogen for reuse.
- Steam reformer synthesis gas
- Refinery and petrochemical gases
- Methanol cracker synthesis gas
- Ethylene cracker gas
- Coke oven gas
- Other hydrogen-rich industrial streams
- High-purity hydrogen production
- High hydrogen recovery
- Load-following operation
- Product purity control
- Reduced switching valve complexity
- Maintenance flexibility
- Finite Element Analysis of adsorber vessels
- Long-term operational reliability
High-purity hydrogen for electrolyser applications
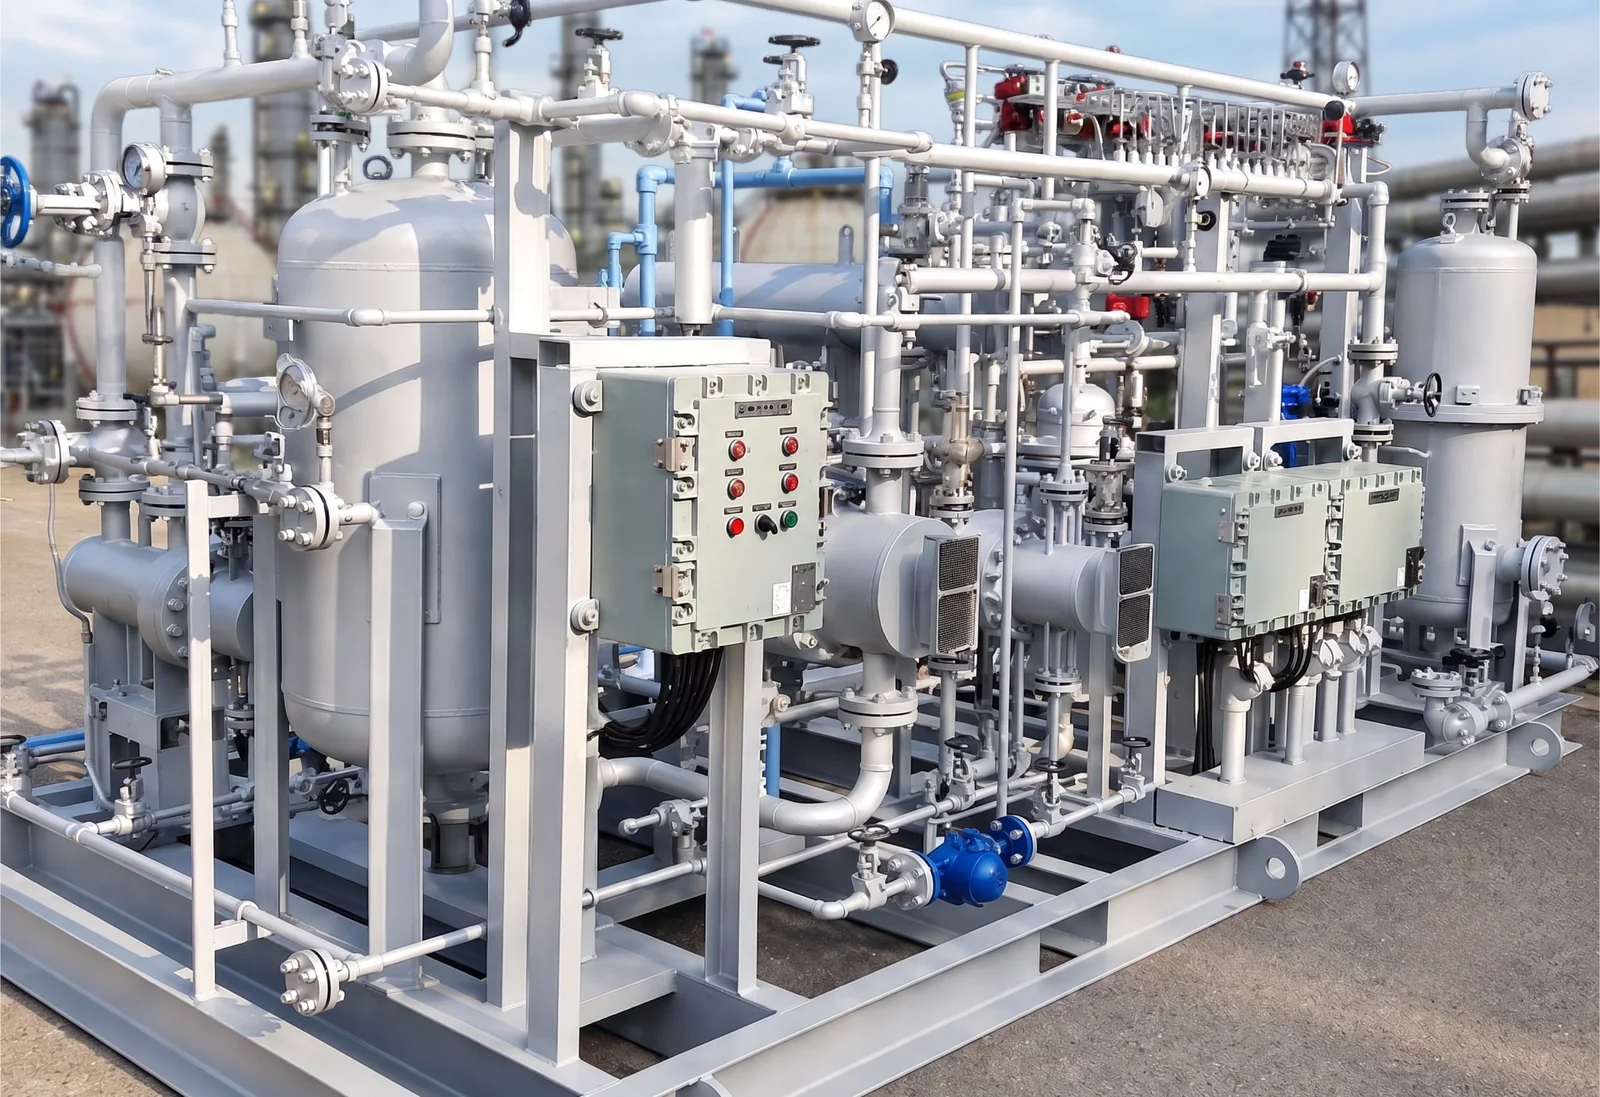
Hydrogen produced through electrolysis may require further purification before it meets the specifications required by downstream processes. Howe-Baker provides modular De-Oxo TSA Dryer systems specifically designed to remove residual oxygen and moisture from hydrogen streams.
The process combines catalytic deoxygenation with Temperature Swing Adsorption, producing hydrogen with purity exceeding 99.999% and reducing residual oxygen to below 5 ppm. Systems can support capacities from approximately 50 to 20,000 Nm³/h, making the technology suitable for applications ranging from smaller installations to large industrial green hydrogen facilities.
- Hydrogen purity exceeding 99.999%
- Residual oxygen below 5 ppm
- Low hydrogen loss
- Compact skid-mounted configurations
- Continuous twin-bed TSA operation
- Scalable system capacities
- Integration with electrolyser packages
- Turnkey engineering around project requirements
Proven hydrogen production with a lower-carbon pathway
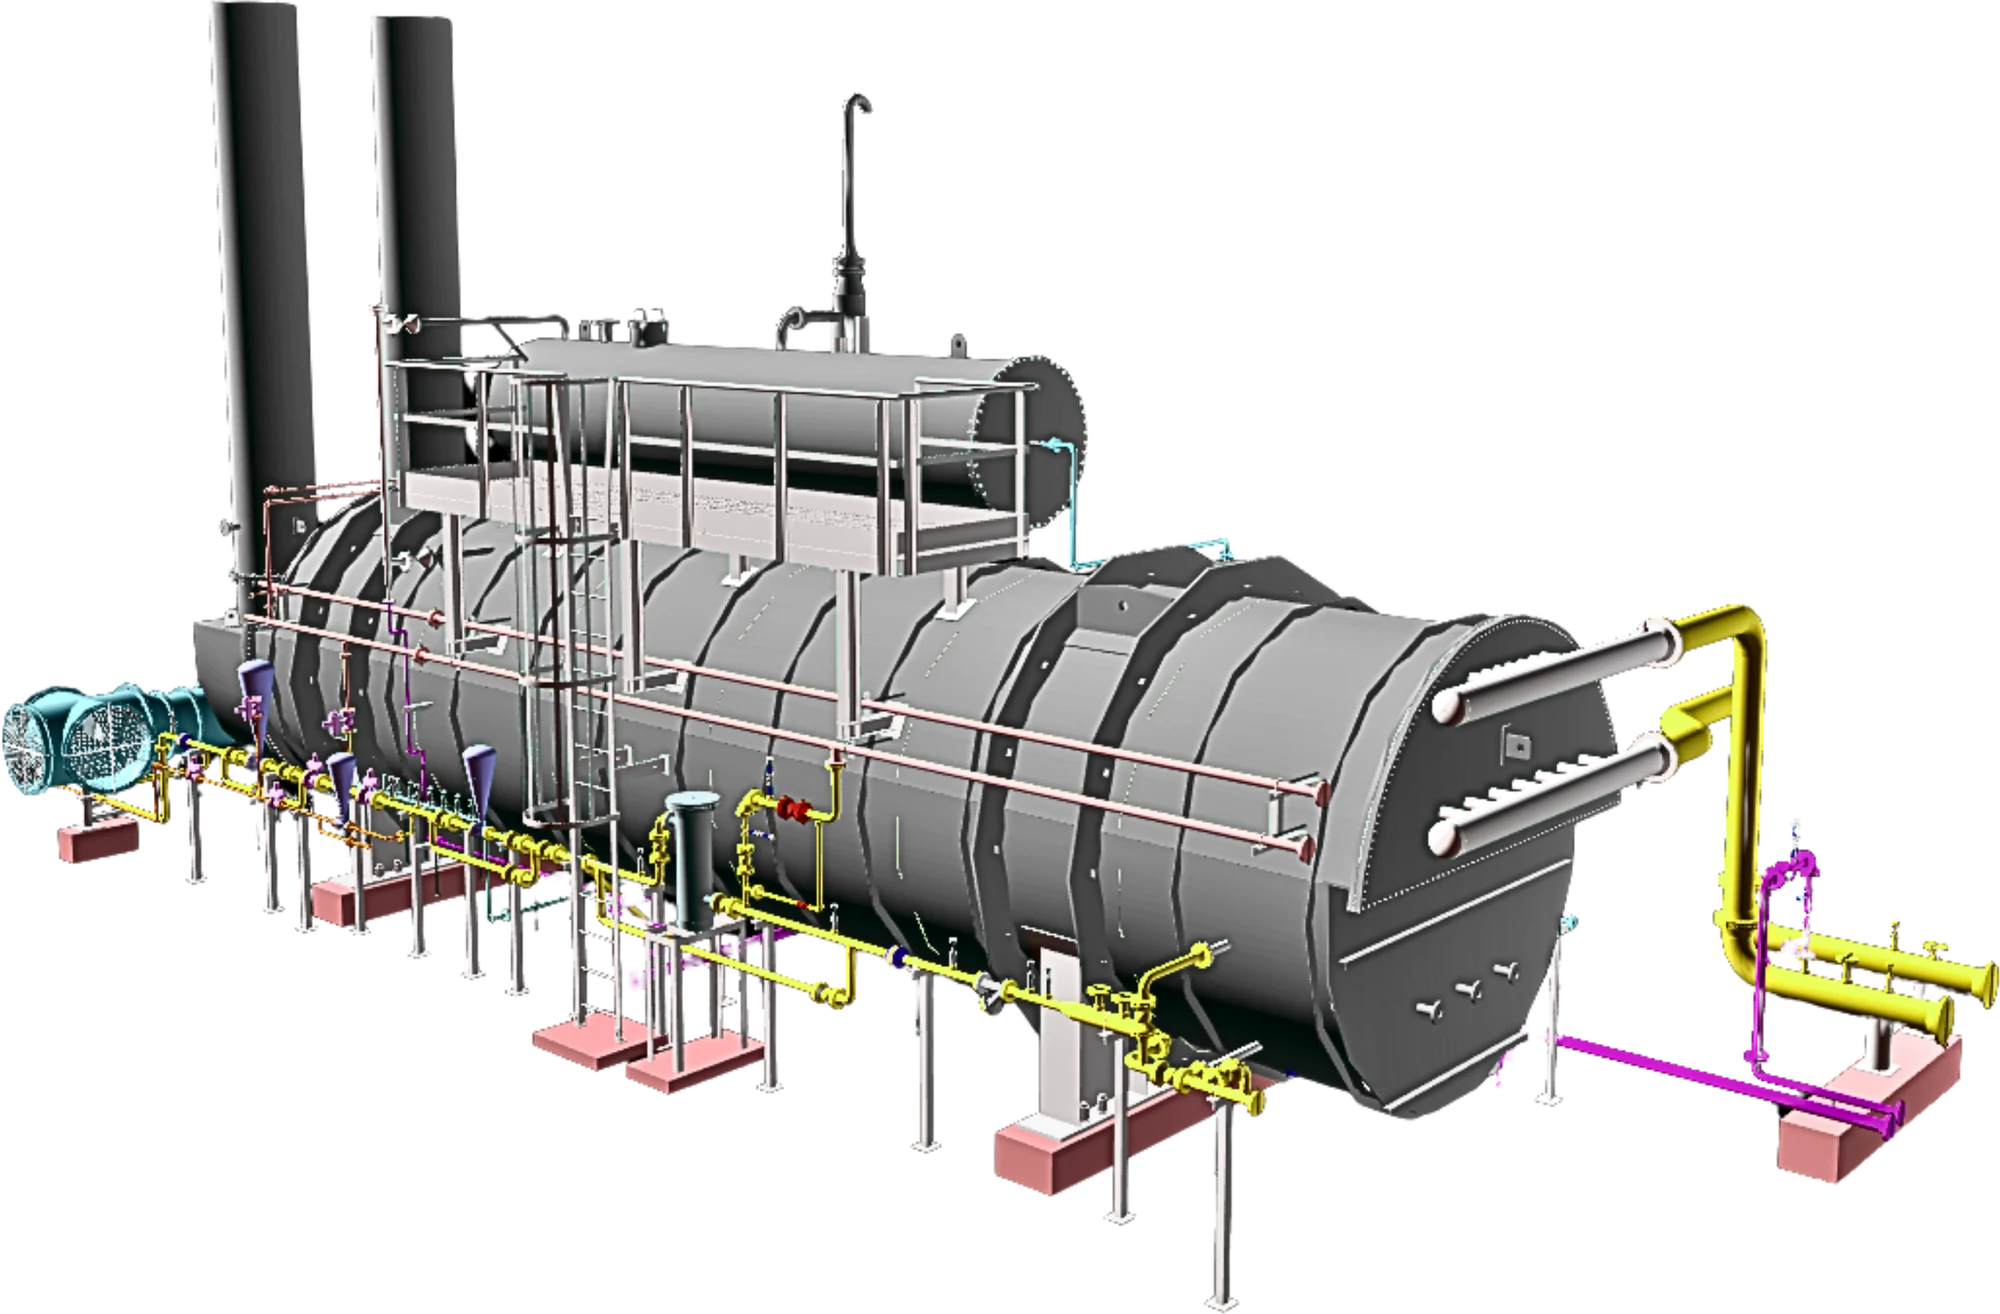
Steam reforming remains one of the world's most established technologies for industrial hydrogen production. Howe-Baker specialises in round furnace steam reformers for small and medium-scale hydrogen production, integrating modern reforming technology with high-performance PSA purification.
The modular nature of round reformers allows significant fabrication to take place away from the final installation site, supporting controlled manufacturing quality, reduced site construction and efficient project delivery. For blue hydrogen projects, this established production and purification expertise provides the hydrogen process foundation for integration into a wider lower-carbon facility.
- Energy efficiency
- Hydrogen recovery
- Reliability
- Emissions performance
- Operational flexibility
- Plant lifecycle performance
Unlock more performance from existing hydrogen assets
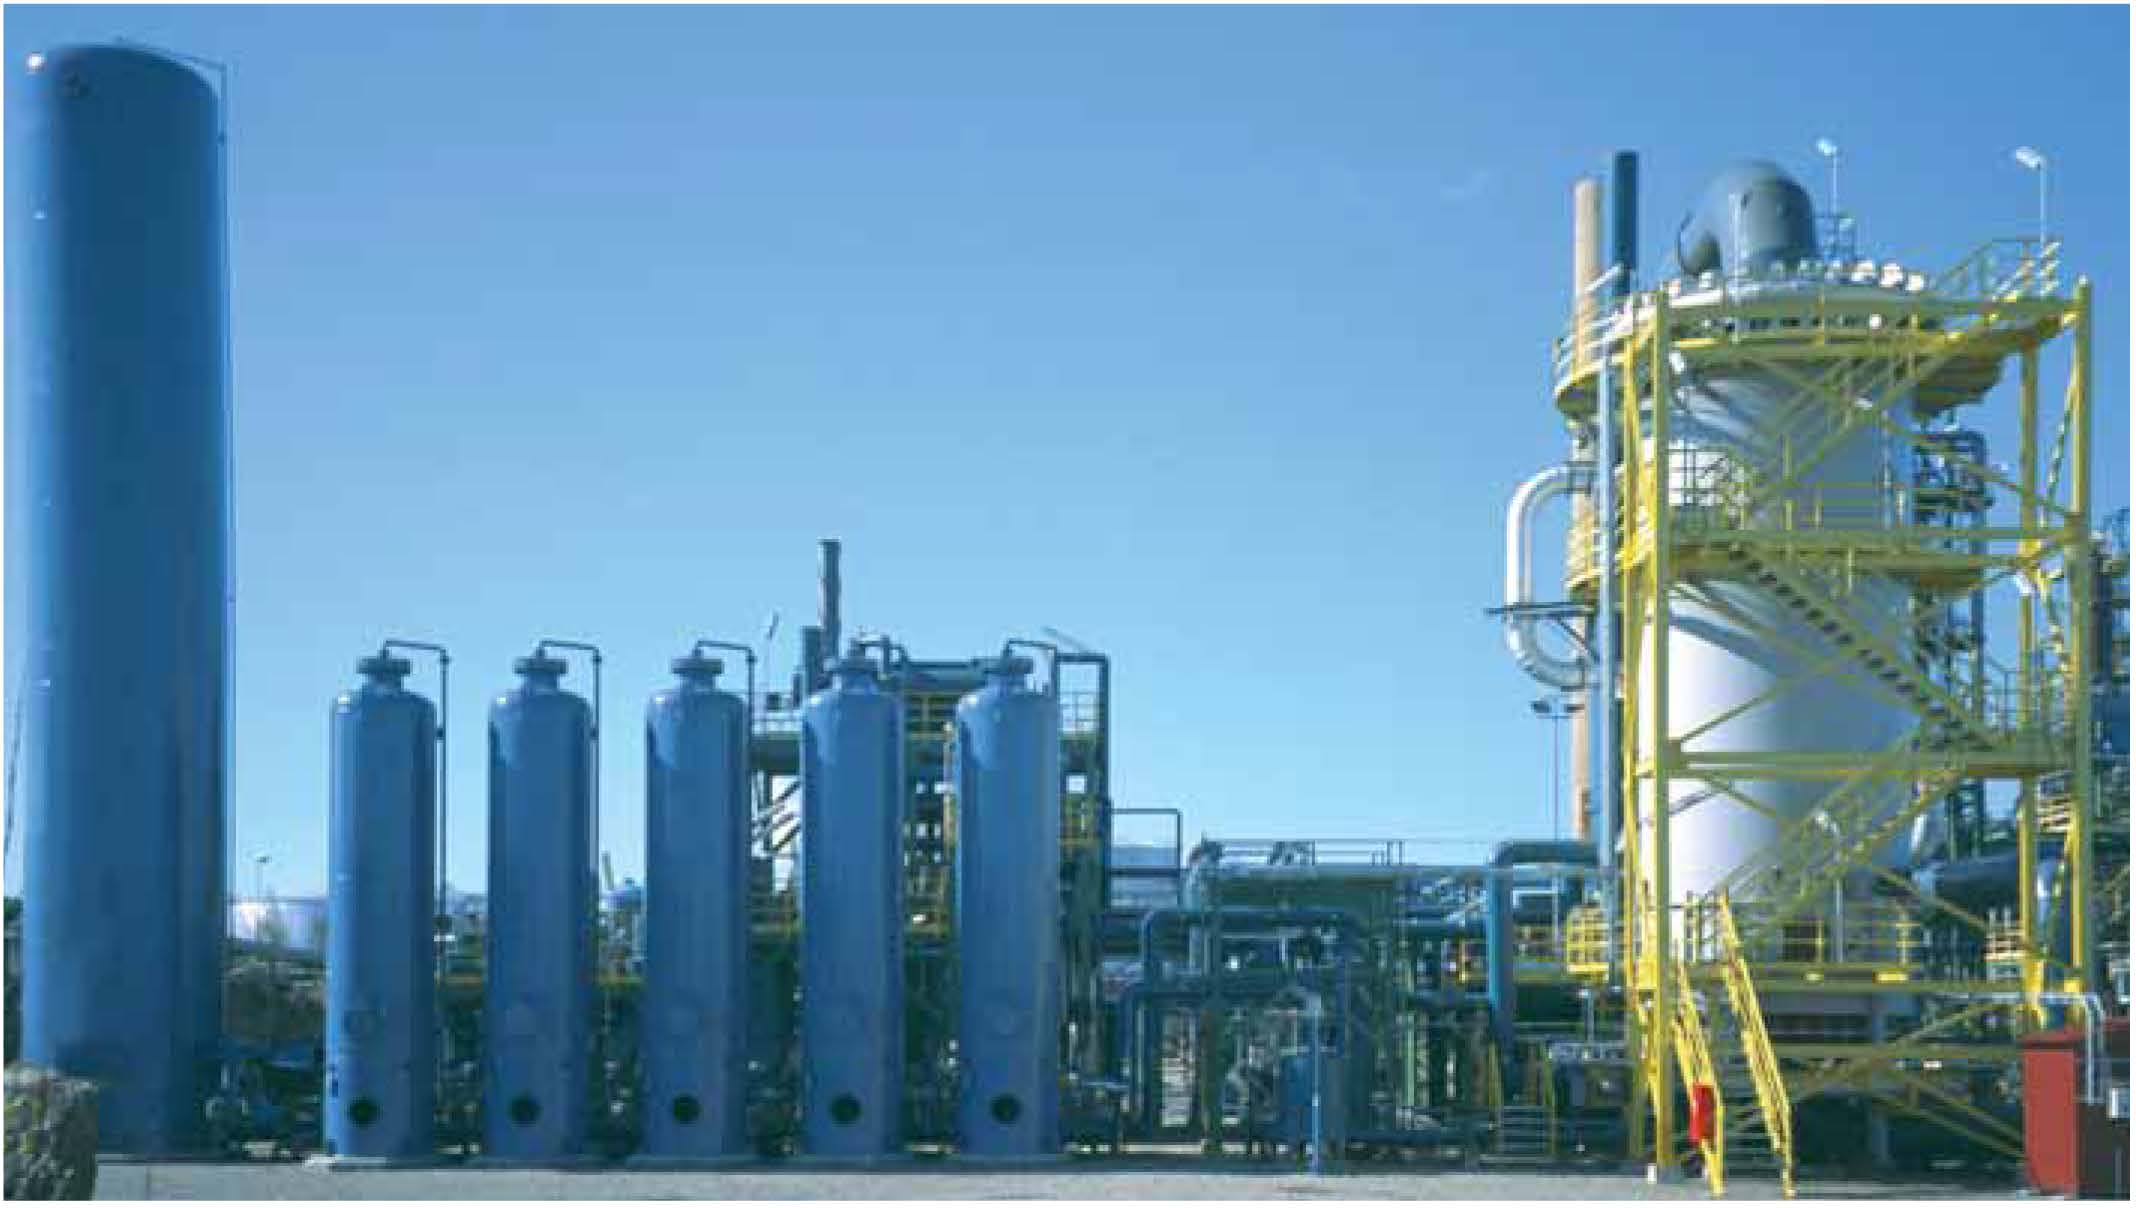
Many hydrogen plants operating today have been in service for decades. Ageing reformer tubes, headers, catalysts, boiler economisers, PSA systems and other equipment eventually require replacement. At the same time, older facilities may contain technologies and design approaches that limit efficiency, reliability or hydrogen recovery.
Rather than simply replacing ageing equipment like-for-like, Howe-Baker evaluates the performance of the complete hydrogen facility. Historical operating data, process simulation and heat-transfer modelling can be used to identify bottlenecks and opportunities to improve the plant.
- Increase hydrogen production
- Improve hydrogen recovery
- Reduce feedstock consumption
- Improve energy efficiency
- Remove process bottlenecks
- Modernise PSA technology
- Upgrade ageing equipment
- Improve reliability and maintainability
- Extend plant operating life
Modern PSA technology can be particularly valuable when upgrading older hydrogen plants, improving recovery while reducing system complexity and potentially increasing available hydrogen production from the existing facility.
Beyond the production plant
Howe-Baker's experience extends beyond hydrogen production and purification into high-pressure hydrogen systems. Projects have included hydrogen systems operating at pressures up to 875 bar, enabling the hydrogen system to be considered from generation and recovery through purification, storage and downstream use.
- Hydrogen compression
- Tube trailer filling and unloading
- Cascade storage
- Industrial hydrogen dispensing
- 350 bar hydrogen systems
- Components and systems for 700 bar applications
- Transportable hydrogen packages
- Controls, telemetry and safety systems
Production. Recovery. Purification. Optimisation.
Howe-Baker brings established process engineering expertise together with technologies designed for the changing hydrogen landscape. Our approach starts with the performance of the complete system.
Hydrogen Recovery
Recover and purify hydrogen from refinery, petrochemical and industrial process streams.
Green Hydrogen
Purification and conditioning of electrolyser-produced hydrogen using De-Oxo and TSA technology.
Blue Hydrogen
Steam reforming and PSA expertise supporting lower-carbon hydrogen production facilities.
Plant Optimisation
Revamps, expansions and modernisation designed to improve the performance and lifecycle of existing hydrogen assets.
Hydrogen projects, delivered
SMR Hydrogen Plant PSA
Texas, USA · North America
High-purity H₂ recovery PSA system for a steam methane reformer — 99.9%+ purity to pipeline specification.
Learn moreRefinery Hydrogen Recovery
Rotterdam, Netherlands · Europe
PSA unit recovering hydrogen from refinery off-gas streams for reuse in hydroprocessing.
Learn moreGreen Hydrogen Purification
North Sea, UK · Europe
TSA De-Oxo followed by PSA polishing for electrolyser output — qualified to ISO 14687 grid quality.
Learn moreDiscuss Your Hydrogen Project
From new hydrogen infrastructure to the optimisation of existing assets, Howe-Baker provides the engineering experience and process technologies required to develop reliable, efficient hydrogen solutions. Talk to our engineering team about your hydrogen requirements.
Talk to our engineering team